
Welding Wire and Heat Input - WELDING-WIRE=HEAT-I
Author: hirocherry7312Executions: 47928
※ This library was created by a member. This site is not responsible for its content.
Heat input Q (J/cm), welding speed s (cm/sec), welding voltage E (V), welding current I (A)
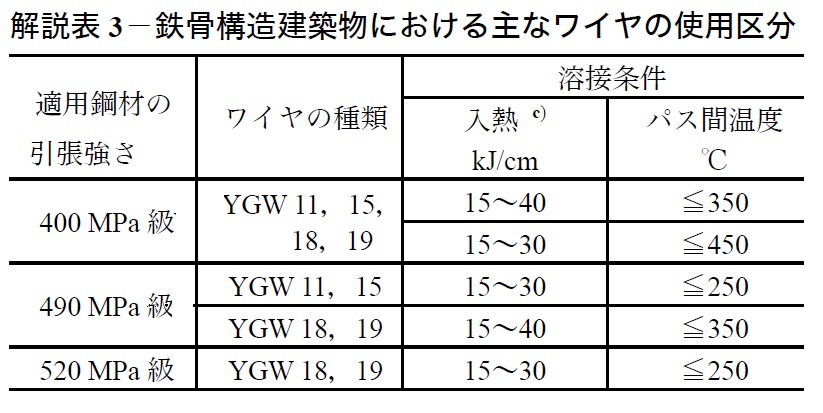
As shown in the figure on the right, Table 3 of the JIS Z 3312 Explanatory Notes lists the heat input (kJ/cm) and interpass temperature (°C) for applicable steel grades with tensile strengths of 400 MPa, 490 MPa, and 520 MPa.
As shown in the figure on the right, Table 3 of the JIS Z 3312 Explanatory Notes lists the heat input (kJ/cm) and interpass temperature (°C) for applicable steel grades with tensile strengths of 400 MPa, 490 MPa, and 520 MPa.
| Q | J/cm |
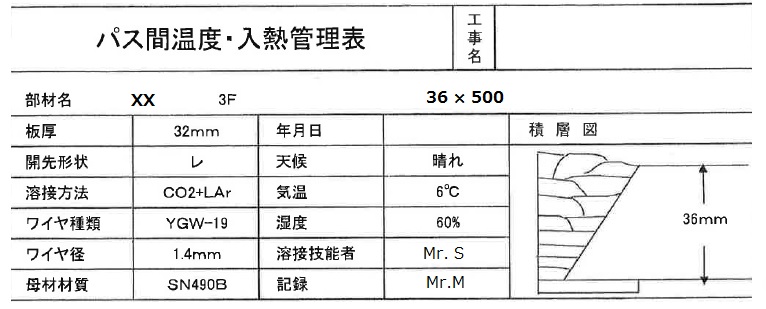
The default value is the fifth pass in the layered diagram shown below.
Note that this cannot be applied to robotic welding.
Note that this cannot be applied to robotic welding.
No customer feedback for this calculation yet.
The heat input is calculated for each pass shown in the layered diagram. This is a critically important welding parameter.
[110,325] WELDING-WIRE=HEAT-INPUT
Q = 60 × Ebolt × Iampere/s